
On a connector, the tolerance that matters is not the one on your drawing — it is the one that
stacks up vertically between your PCB, the contact, and the mating half.
This is how we control it, and how we prove it.
Tolerance Stack-Up: Where Interconnects Actually Fail
A contact can pass every individual dimension
Critical dimensions, functional consequence and how we verify them
The bands below are the normal production tolerances we hold — not a marketing claim. They are what we can defend in a first-article report, batch after batch. Where a drawing calls for something tighter or looser, that is a DFM conversation rather than a catalogue lookup.
| Dimension | Standard production | Precision grade | Consequence if it drifts | How we verify |
|---|---|---|---|---|
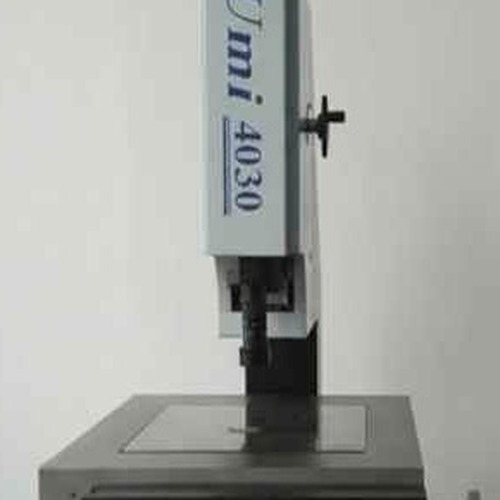
| Pitch (contact-to-contact spacing) | ±0.05 mm | ±0.03 mm | Off-pitch accumulation across a long row; high insertion force at the far end | Vision measuring system, full-row scan |
| Contact position height | ±0.05 mm | ±0.03 mm | Insufficient working stroke; intermittent contact or open circuit | Vision measuring system, against datum |
| True position of contact point | ±0.05 mm | ±0.03 mm | Lateral misalignment with the mating pin; contact resistance rise | Vision measuring system, projected contact point |
| Plating thickness (Au) | 1–30 µ″ selectable | — | Wear-through, corrosion, unstable contact resistance | Plating thickness measurement, incoming lots |
| Plating thickness (Ni underlayer) | 50–100 µ″ | — | Poor barrier function; interdiffusion under thermal load | Plating thickness measurement, incoming lots |
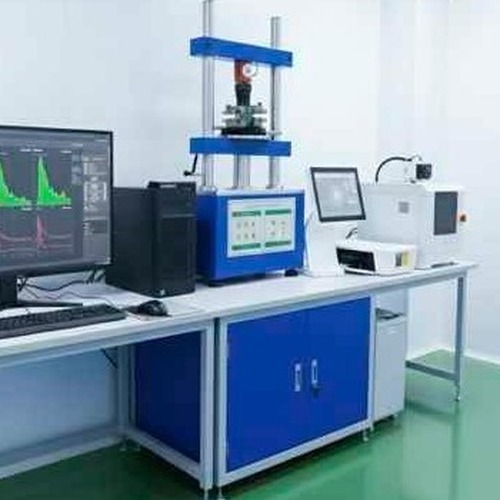
| Insertion / withdrawal force | Per drawing requirement | — | Too high → tooling and operator damage; too low → retention risk | Connector force tester, with the specified mating pin |
| Contact resistance | Per drawing requirement | — | Localised heating; signal integrity degradation | DC low resistance measurement, at specified current |
| Stroke / working travel | Per drawing requirement | — | Bottoming out, or loss of spring pre-load | Vision measuring system combined with force tester |
One number is published deliberately, rather than a range applied across every part number. A blanket tolerance is not a specification — it is a liability.
Responsibility boundary across the four contributors
| Stack-up contribution | Who owns the geometry | What Jiatel controls | What we need from you |
|---|---|---|---|
| Board-side (pad, drill, finish) | Customer design | Nothing — reviewed and flagged during DFM | Pad data and position tolerance |
| Contact-side (terminal geometry) | Jiatel — in-house stamping, forming and assembly | Tooling, forming, in-process measurement, final QC | Mating-cycle target and force requirements |
| Mating-side (counterpart part) | Customer / third party | Nothing — but we model its contribution during DFM | Counterpart drawing and position tolerance |
| Assembly / process | Shared | DFM support and first-article verification | Assembly method (SMT, THT, wire, potting) |
Making this boundary explicit is not an attempt to move responsibility. It is the only way to close a stack-up: if the mating-side contribution is unknown, the total is unknown, and the tolerance on our side has to absorb a number nobody has calculated.
on its drawing and still fail in the assembly. The reason is almost always cumulative vertical tolerance — three independent contributors that add together.
Board-side tolerance
PCB thickness variation, pad finish height and solder-joint height. Typically the contributor you control least — which is why we take it as given rather than as a variable.
Contact-side tolerance
Stamped metal thickness, formed height, and plating build-up. This is the contributor we own on the press — and the one we hold tightest.
Mating-side tolerance
Mating half position, housing datum and insertion depth. Determines how much working stroke you actually have left.
How We Control It
Tolerance control on a connector is a press-and-die discipline before it is an inspection discipline.
- Stack-up review before toolingWe model the three contributors using your board thickness as an input, and confirm the remaining working stroke in writing — before any tooling is cut.
- Die and forming controlForming height is held at the press, with in-process checks on the stamping line rather than a final gate only.
- Plating build-up accounted forGold thickness is a dimensional contributor, not just a cosmetic one. It is specified and measured, not assumed.
- Measured verification, not visualDimensional verification on a vision measuring system, with measured values in the first article report.
Plating is an outsourced step — and how we control it
Plating is outsourced. We do not operate a plating line and we do not describe it as in-house. What we do control is the specification and the incoming verification: gold thickness selectable 1–30 µ″ with a nickel underlayer of 50–100 µ″, thickness verified by measurement on incoming lots rather than by supplier certificate alone, appearance and adhesion criteria applied at incoming inspection, and batch traceability retained so a plating deviation can be traced to a specific lot.
Being explicit here is deliberate. An outsourced step that is openly described and measured is a lower risk than an in-house step that is only assumed.
Force is only meaningful as a pair
Insertion and withdrawal force are set by spring geometry and stroke, and are verified with a connector force tester against the drawing requirement. Because force is a function of the mating pin as well as of the contact, verification is only meaningful when our part is measured against the counterpart geometry it will actually meet. A force figure quoted without its mating pin and its measurement stroke is not a specification.
The Instruments Behind the Numbers
These are the measurements behind every claim we make on a datasheet.
Measurement capability and what each instrument is used for
| Instrument | What it measures | Measurement definition |
|---|---|---|
| Vision measuring system (VMS) | Pitch, position height, true position, row accumulation, overall dimensions | Measured against the drawing datum — not against the part edge |
| Connector force tester | Insertion force, withdrawal force, spring force at working stroke | Measured with the specified mating pin, at the specified stroke |
| DC low resistance measurement | Contact resistance | Measured at the specified current and after the specified mating cycles |
| Life cycle durability rig | Contact resistance and force retention against cycle count | Measured under standard laboratory conditions (25 °C, 50 % RH) |
Dimension and appearance: 100 % AOI on production. This is the part of the tolerance chain where sampling is not acceptable, because a mis-formed or off-pitch contact is a single-part failure rather than a population failure. Mechanical and electrical characteristics: sampling at AQL 0.65, with force and contact resistance as the controlling characteristics.
m for dimensional verification”> Dimensional & tolerance verificationVision Measuring (VMS)
Connector Force Tester
Insertion / withdrawal force
DC Low Resistance
<30mΩ contact resistance
Life Cycle Durability
100,
Current-carrying capacity
We do not publish a single current rating for a contact family, because the number depends on the mating pin, the housing, the PCB copper and the ambient condition. A rating without its test conditions is not a specification. Our published position is:
Subject to specific mating pin and housing design. Test reports available upon request.
Life cycle
Contact resistance and normal force both change with cycle count, and the rate depends on the mating surface rather than on the contact alone. Our published position is:
Tested under standard laboratory conditions (25 °C, 50 % RH) with specific mating surfaces. Life cycle varies by application.
Verification and acceptance basis
| Item | Inspection basis | Acceptance basis | Note |
|---|---|---|---|
| Dimensions and appearance | 100 % AOI on production | Against drawing datum; precision grade ±0.03 mm where specified | Single-part failure mode — no sampling |
| Plating thickness | Incoming lot measurement | Au 1–30 µ″, Ni 50–100 µ″ | Supplier certificate alone is not sufficient |
| Insertion / withdrawal force | AQL 0.65 sampling | Against drawing, with the intended mating pin | Force is only meaningful as a pair |
| Contact resistance | AQL 0.65 sampling | Against drawing, at the specified current | Reported with its test current |
| Life cycle | Per agreed test plan | Standard lab conditions (25 °C, 50 % RH), specific mating surfaces | Life cycle varies by application |
| First article | Full dimensional report | All controlling characteristics | Issued before volume ramp |
000+ mating cycles
Tolerance Under Stress
Tolerance that holds at 25°C is not the same as tolerance that holds after thermal cycling, humidity and corrosion.
Tolerance Questions Engineers Ask
What dimensional tolerance can you hold on a stamped contact?
It depends on the feature and the material thickness. Send the drawing and we will confirm, feature by feature, what the die can hold — in writing, before tooling. We would rather decline a tolerance we cannot hold than ship to it and sort later.
Why won’t you quote one tolerance for every part?
Because the tolerance a part can hold depends on its geometry, its material thickness and the tooling used. A single site-wide number would be either looser than we achieve on some parts, or unachievable on others. Where a part genuinely can hold a wider band, we will say so — and where it cannot, we will say that too.
Does plating thickness count toward the tolerance chain?
Yes, and it is commonly forgotten. Plating build-up is a contributor to the contact point position when measured at the contact face, which is why plating thickness is measured on incoming lots rather than assumed from a supplier certificate.
Who is responsible for the mating-side contribution?
It sits in your design and we cannot measure it from our side. Send the counterpart drawing and we will model its contribution during DFM, so that the number our tolerance has to absorb is a calculated one rather than an assumed one.
What happens if the stack-up fails at first article?
We re-measure every controlling characteristic against the drawing datum and separate our contribution from the mating-side and board-side contributions. If the deviation is ours, the corrective action is tooling or fixturing — not a renegotiation of the tolerance.
How do you handle tolerance stack-up with my PCB?
We take your board thickness and mounting type as inputs, model the vertical contributors, and return the remaining working stroke. This is part of the DFM review and is included with the quote.
Is the gold plating thickness included in the dimensional calculation?
Yes. Plating build-up is a dimensional contributor on the contact face, so it is specified and measured as part of the geometry — not treated as a separate finish-only concern.
Do you provide measured values or just pass/fail?
Measured values. First article reports carry the actual measured numbers, not a checkbox, so your team can compare them against your own stack-up.
Send your stack-up. Get a tolerance review in 12 hours.
Our engineer will confirm working stroke, flag stack-up risk, and quote from USD 600 tooling.